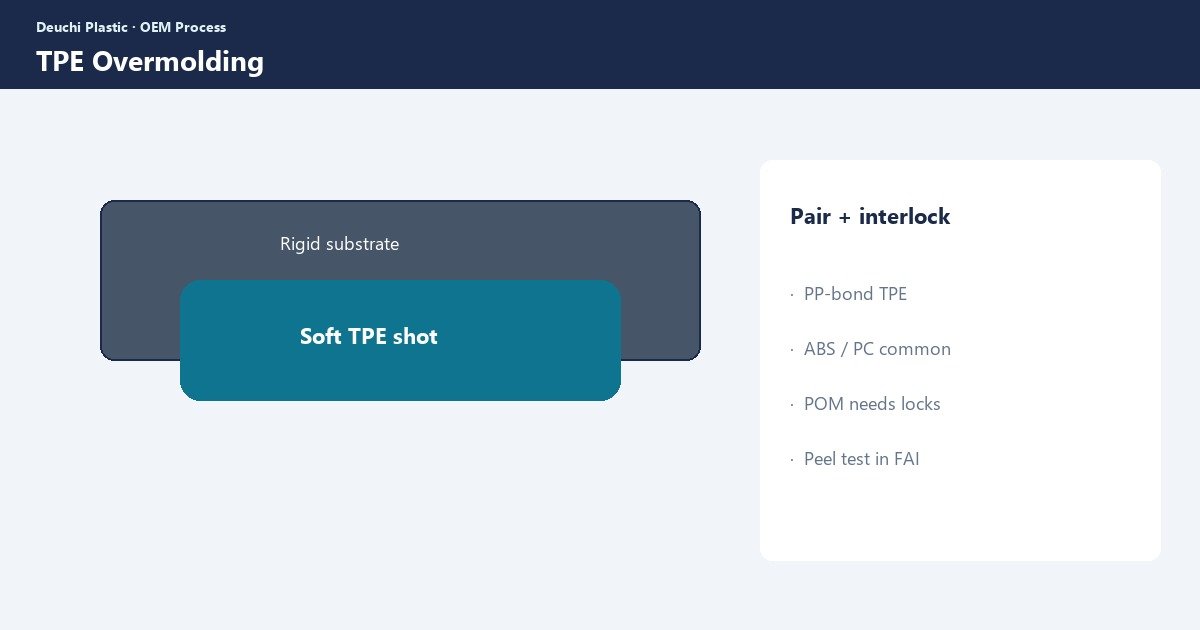
TPE overmolding is how OEMs put a soft grip, seal, or button on a rigid substrate without a second fastener. It fails when the pair does not bond, the shutoff flashes, or the soft shot shrinks off a sharp corner. “TPE” is a family — SEBS, TPU, and others are not drop-in equivalents.
This guide is the OEM pair-and-tool version. General process: overmolding injection molding. When volume justifies a 2K cell: two-shot.
Substrate pairs that usually work — and that do not
| Substrate | TPE / TPU note | OEM caution |
|---|---|---|
| PP | Common with PP-bond TPEs | Need the grade sold for PP; mechanical interlock still helps |
| ABS, PC/ABS, PC | Many TPEs bond; TPU common for abrasion | Residual stress + chemicals — ABS, PC |
| PA / GF nylon | Harder; specialized grades or primer | Moisture and warp — GF nylon |
| POM | Poor chemical bond | Design interlocks; do not trust ads — POM |
Name both grades. Shore A, color, and UV/oil duty belong on the RFQ. A “soft TPE” without chemistry is not a spec.
Bond vs interlock
- Chemical bond: clean substrate, right melt, right pair, no mold release on the interface
- Mechanical interlock: holes, grooves, undercuts — actions may be required
- Peel test and environment (sweat, oil, heat) in the quality plan, not “it stuck at T1”
Shutoffs control flash of the soft shot: flash. Substrate tolerance is now a shutoff dimension — tolerance.
Transfer overmold vs two-shot
| Transfer / pick-and-place | Two-shot (2K) | |
|---|---|---|
| Tooling cost | Lower entry | Higher |
| Registration | Depends on nest and substrate consistency | Usually better |
| Volume | NPI and mid | High, stable pair |
Inserts and metals are a different process: insert molding. Do not mix the words on an RFQ.
DFM for the soft shot
- Avoid razor-thin TPE tips that tear on eject — pin strategy: ejector marks
- Give the TPE a path; weld lines in a seal bead leak — weld lines
- Draft the soft face; TPE sticks
- Do not paint the substrate in the bond zone
Written DFM: checklist. Sample gates should include peel or leak tests: T0–T2.
How Deuchi quotes TPE overmold
Deuchi quotes the pair, shutoff concept, and whether transfer or 2K is honest for the volume. We will recommend interlocks when the chemistry is weak (POM, some nylons). Contract manufacturing; send CAD and Shore target via contact.
FAQ
Is TPU the same as TPE?
TPU is a type of thermoplastic elastomer. Abrasion and oil resistance differ. Specify chemistry, not only Shore A.
Can we overmold onto printed logos?
Ink in the bond zone is a contamination risk. Keep graphics off the interface.
Why did the grip peel after a month?
Wrong pair, residual stress, oil/sweat, or no interlock. Re-qualify the pair; do not only “turn up heat.”
Do we need a primer?
Some nylon and specialty substrates yes. Primer is a process step with its own control plan.
Next step: Contact Deuchi with both CAD bodies, substrate grade, TPE/TPU target, and whether the joint is grip or seal.